
About Rupal Colorchem Industries
Founded in 2010, Rupal Colorchem Industries (RCI) is a globally recognized manufacturer and exporter of premium industrial dyes. We specialize in Direct Dyes, Acid Dyes, Solvent Dyes, and Basic Dyes, catering to industries where color quality, consistency, and sustainability are critical—such as textiles, leather, food, paper, plastics, and specialty applications.
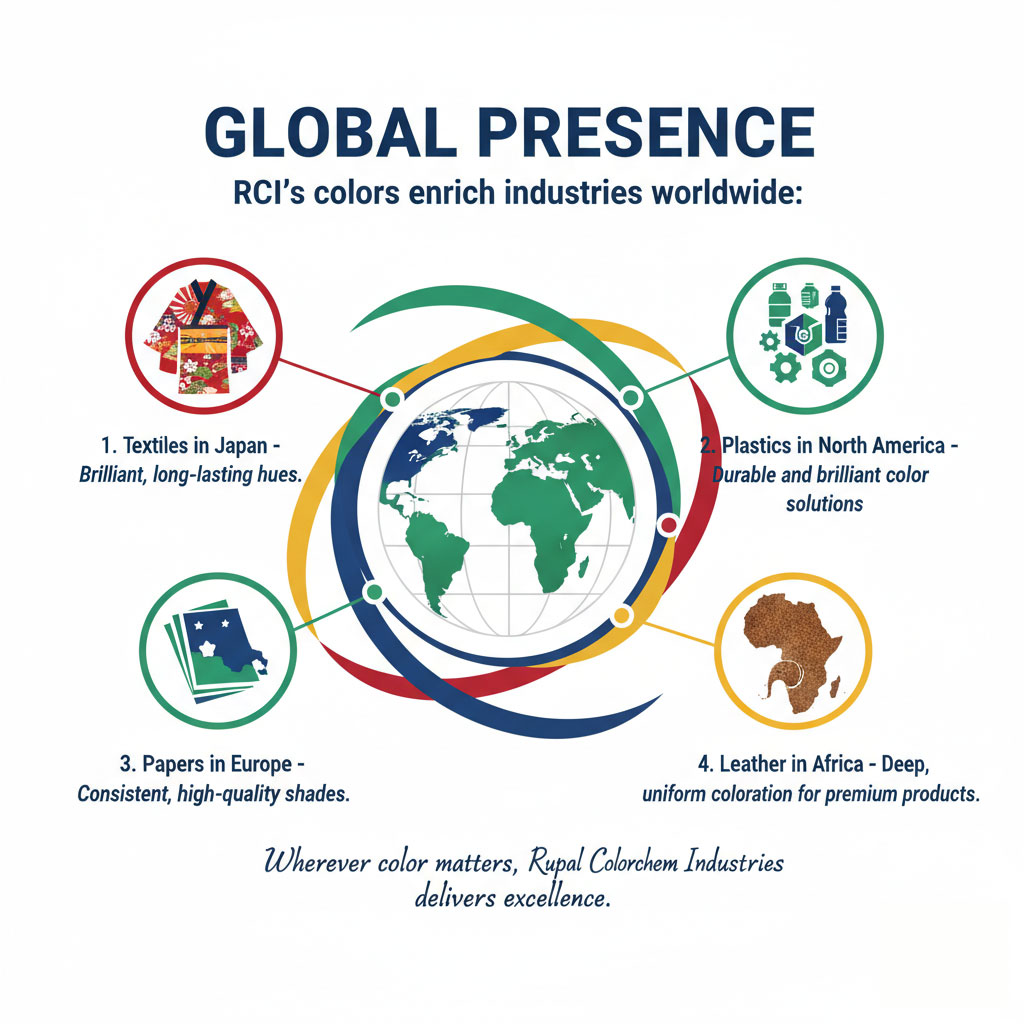
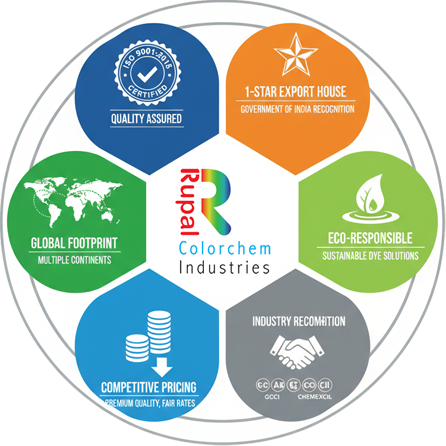
With a strong presence in USA, Japan, China, UK, Canada, Egypt, Africa, and Australia, RCI is trusted by global clients for reliable performance, consistent quality, and exceptional value. Each dye solution is crafted to enhance product appeal, brand identity, and customer satisfaction.
Vibrant shades for textiles and paper, ensuring long-lasting color retention.
Perfect for leather, wool, nylon, and silk, delivering deep, even coloration.
Stable and bright dyes for plastics, fuels, coatings, and polymers.
Intense, durable colors for acrylic fibers, inks, and specialty applications.
All products undergo rigorous testing in state-of-the-art laboratories to meet global quality standards and compliance.
Why Choose RCI?
Durable, vibrant dyes for fabrics and garments.
Deep, uniform coloration for high-quality leather products.
Safe, compliant color solutions.
Bright, consistent shades for all types of paper.
Stable, color-rich solutions for industrial use.
Custom dyes for unique industry requirements.